Reamers
Ask your agent to find products in Reamers. Your agent finds and compares. You approve the buy. Connect your agent
Sellers list 5 products in Reamers on CommerceBook. Updated November 14, 2026.
Browse the products
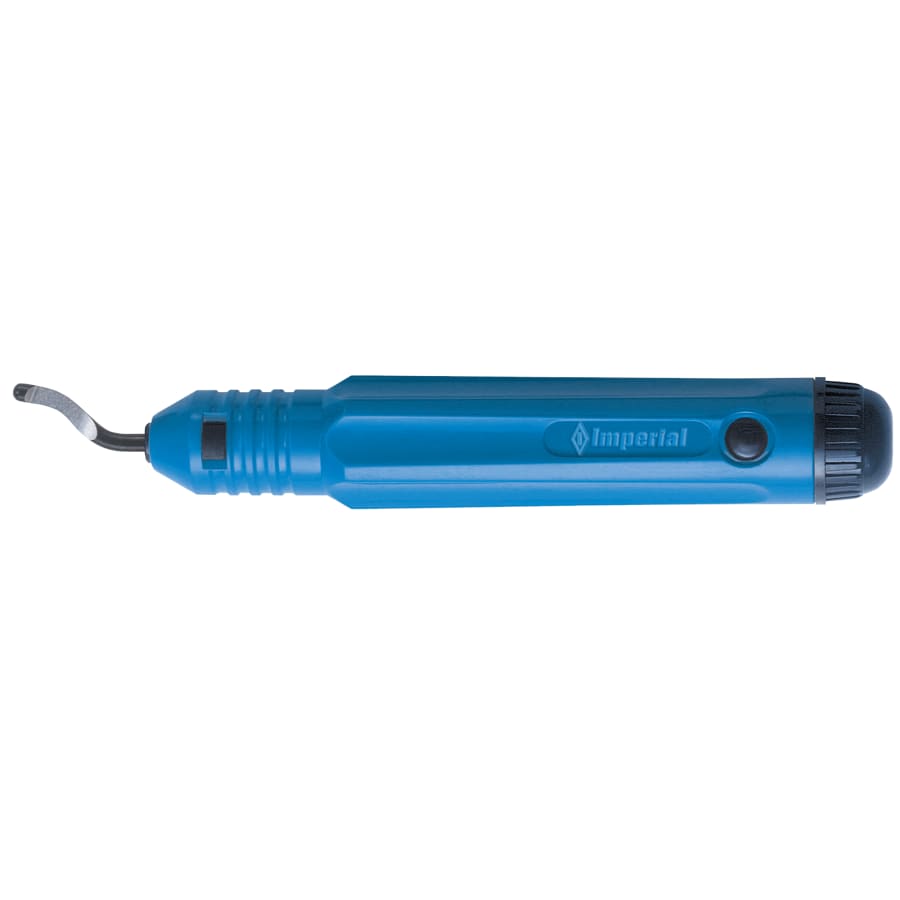 Imperial Tool manual deburring tool, model 210-FImperial Tool$47.99 USD each
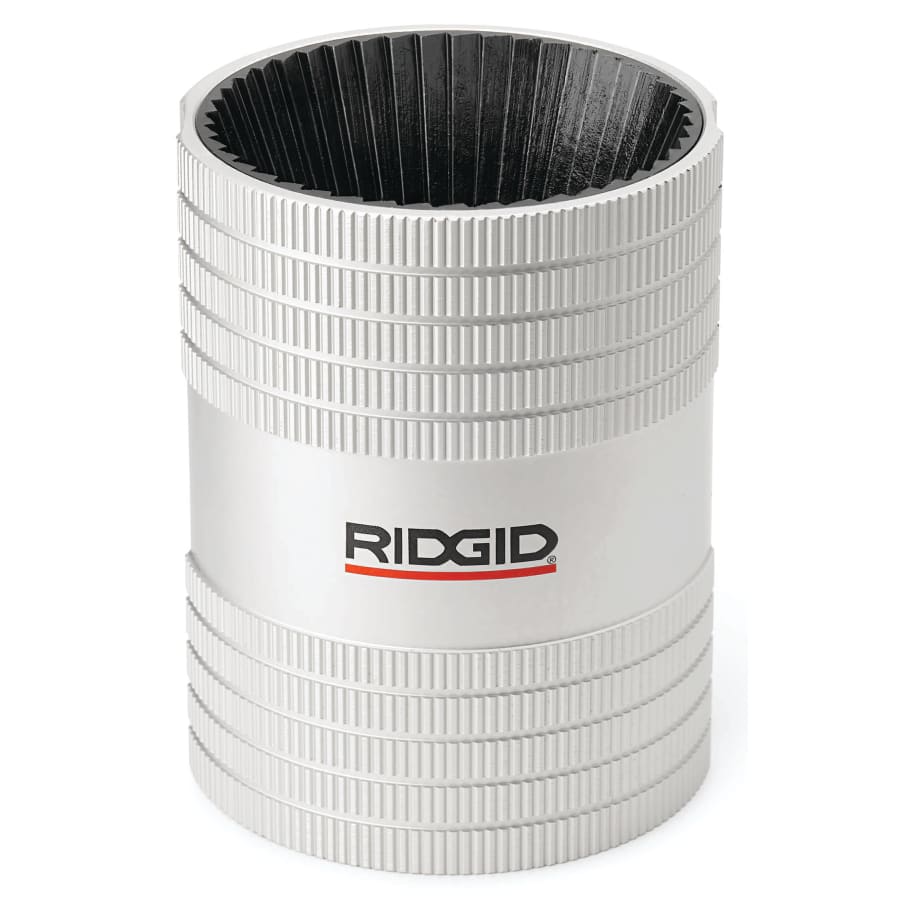 RIDGID 227S reamer, manual, model 29993RIDGID$187.99 USD each
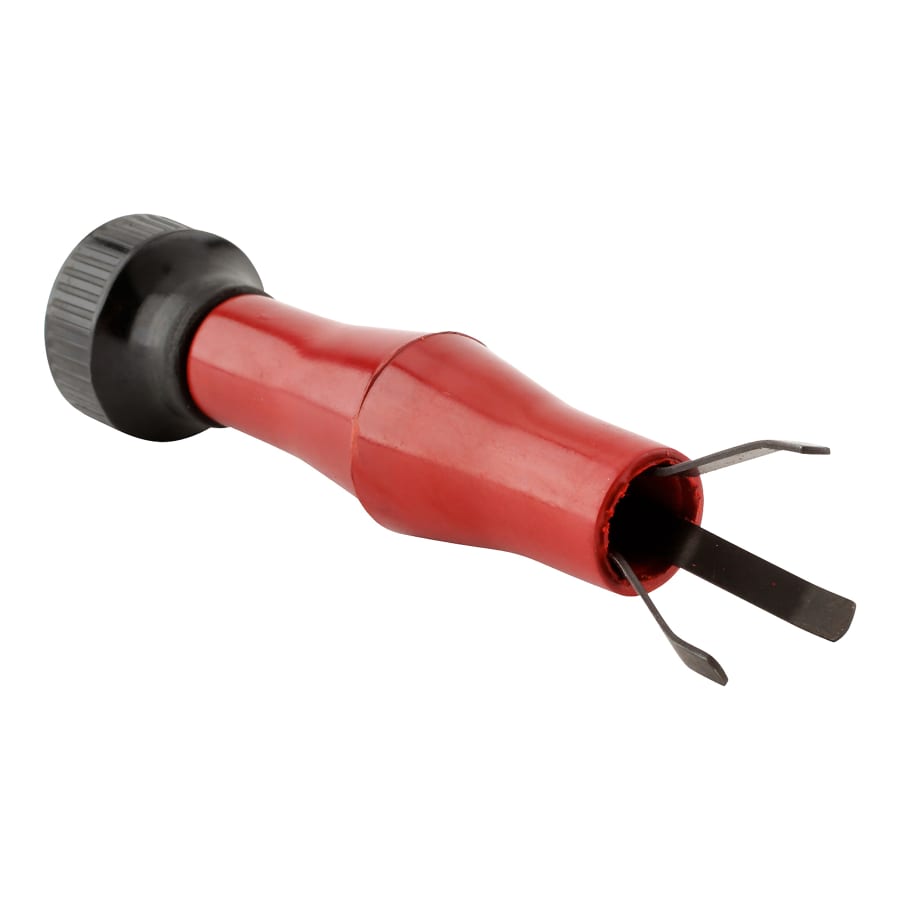 Harris Product Group nozzle reamer, manual, model 3060030Harris Product Group$40.99 USD each
- No photo yetRIDGID I/O reamer, 1/4-inch to 1.25-inch, model 29983RIDGID$93.99 USD each
- No photo yetGeneral Tools swivel head deburring tool with 2 blades, model 482General Tools$33.99 USD each
About Reamers
Reamers are hardware tools that finish or enlarge drilled holes. The buyer checks the hardware material before buying. The buyer checks the color and the pattern of the item. The buyer checks if the reamer works with the materials in the project. The buyer checks for compatibility with metals, steel, and iron. The buyer checks the tool type and the size. The buyer checks the machining environment and the long term value. The buyer checks the setup and the fixturing for possible alignment causes. The maker specifies a reamer with a positive radial rake to reduce cutting pressure. The buyer verifies feeds and speeds to prevent tapered holes.
Read what buyers ask
What materials can reamers work with?
Reamers are capable of working with metals, steel, and iron. They are typically only used on metals and are not compatible with plastics.
What causes oversized or tapered holes?
Misalignment and incorrect feed or speed cause oversized or tapered holes. The buyer checks fixturing and setup for possible causes.
How does tool wear affect reamer performance?
Excessive tool wear can cause high speed steel reamer holes to grow in size.
Is a reamer a location tool?
A reamer is not a location tool. A chucking reamer will only follow the existing hole.
What are the long term benefits of tapered reamers?
Tapered reamers are an excellent long term value. They can often be reground multiple times while maintaining concentricity and geometry.
How do you size the drilled hole before reaming?
The drill size must be slightly smaller than the desired diameter of the reamed hole. In most cases, the drill size is between two and four percent smaller.
How should you grind a spiral fluted reamer?
You grind a secondary lead angle immediately behind the forty five degree chamfer. You also specify a reamer with a positive radial rake to reduce cutting pressure.